A Beginner's Map to CO2 Laser Materials
The single biggest factor in your success with a CO2 laser is not the machine, it is the material sitting under the beam. Every substrate reacts differently to heat, absorbs infrared light at its own rate, and leaves its own residue behind. Learning a handful of reliable materials well will take you further than owning a giant catalog of exotic blanks you have never tested.
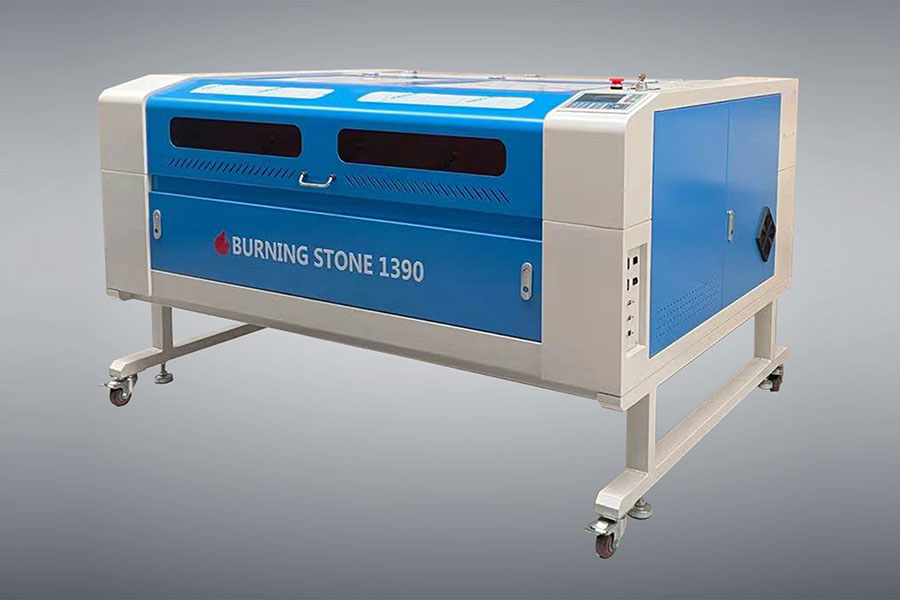
This guide walks through the craft materials that beginners reach for most, the settings that tend to work, and the traps that waste stock. When you are ready to buy a machine sized for these jobs, the options at https://www.redsaillaser.com/Laser-Cutter.html cover everything from small desktop beds to larger flatbeds.
Wood: The Reliable Everyday Favorite
Wood is where most makers start, and for good reason. Plywood, MDF, and solid woods like birch, maple, and bamboo all engrave with a warm contrast and cut cleanly at modest power. Softwoods such as pine cut faster but can scorch, while hardwoods need a bit more energy and reward you with finer detail.
A safe starting point for 3-4 mm Baltic birch plywood is around 35-55% power at 15-25 mm/s for cutting, and 12-20% power at 200-400 mm/s for engraving at 300-500 DPI. Always run a test square, because density varies even between sheets from the same supplier. Masking tape on the surface before engraving keeps soot from staining the wood around the mark.
Sealing is optional but worth knowing. A light coat of linseed oil or clear finish deepens engraved contrast on open-grain woods, while a quick sand after cutting removes the brown edge "kerf kiss" that laser cutting leaves behind.
Acrylic: Glossy Cuts and Frosted Engraves
Cast acrylic is the star of laser cutting because it melts away with a flame-polished, glass-clear edge that no blade can match. Extruded acrylic also cuts but tends to produce a rougher, more melted edge, so cast is preferred for crisp craft pieces. Both engrave to a frosted white look that reads beautifully on clear or colored stock.
For 3 mm cast acrylic, cutting often sits near 45-65% power at 10-20 mm/s, while engraving runs about 20-30% power at 250-400 mm/s. Use lower DPI (around 200-300) for fills to avoid over-melting, and always remove the protective film only after cutting to prevent surface scratches. Push air assist during cuts to blow away molten debris and keep edges clean.
One caution: never laser unknown plastics. If a scrap smells like vinegar or produces black smoke with a greasy film, stop. Some plastics release chlorine gas, which is dangerous and destroys optics.
Leather and Fabric: Soft, Personal, Profitable
Vegetable-tanned leather engraves to a rich, burned-in tone that looks premium on wallets, bookmarks, and tags. Avoid chrome-tanned or treated leathers, which can release harsh fumes and produce uneven marks. For 2-3 mm veg-tan, try 15-25% power at 150-300 mm/s with 300-400 DPI for a controlled etch rather than a deep burn.
Felt and cotton fabrics cut nicely and seal their own edges as they part, which prevents fraying. Keep power moderate and speed higher so you do not scorch beyond the cut line. Natural fibers are safe; synthetic blends may melt instead of cutting and can smell unpleasant, so test a scrap first.
A quick checklist helps you avoid costly mistakes with soft materials:
- Confirm the leather is vegetable-tanned, not chrome or PU-coated.
- Test fabric scraps for melt versus clean cut before a real project.
- Use low air assist on thin leather to avoid blow-away during fine etch.
- Keep a damp cloth nearby in case a fiber edge starts to smolder.
Paper, Cardstock, and Glass: Light Touch Materials
Paper and cardstock are wonderful for invitations, shadow boxes, and layered crafts, but they burn fast. Use very low power (5-12%) and high speed (300-600 mm/s) with multiple light passes rather than one heavy cut. A honeycomb or pinned-down flat surface stops curling and keeps thin sheets from lifting into the beam.
Glass does not cut on a CO2 laser, but it engraves by fracturing the surface into a frosted mark. Clear glass shows marks best when backed with a contrasting material or wetted with a paper towel (the "wet-towel trick" covered in our glass guide). Power around 25-40% at 200-400 mm/s with 300-500 DPI gives a readable etch; too much power just cracks the surface.
Stone, slate, and anodized aluminum also take marks, but slate and anodized coatings are the easy wins for beginners, while bare metals need special treatments and are best left until later.
Materials to Avoid and Why
Some materials are simply unsafe or unrewarding on a CO2 laser, and knowing them protects both you and your machine. PVC and vinyl release chlorine gas that attacks metal parts and your lungs, so they are an absolute no. ABS plastic melts into a gooey mess and smells terrible, and polycarbonate tends to discolor and resist cutting.
Mirrored or reflective metals can bounce the beam back into the lens and cause damage, so bare metal should wait until you understand coating methods. Foam cores with unknown adhesives may off-gas, and anything with a hidden glue layer can surprise you with toxic smoke. When in doubt, burn a tiny corner scrap outdoors first.
The rule of thumb: if you do not know the exact composition, do not cut it inside. Build a labeled shelf of trusted suppliers and stick to materials you have tested. A short list of safe, repeatable blanks beats a risky experiment every time, and it keeps your optics clean and your workshop breathable.
Building a Material Testing Notebook
The fastest way to stop wasting stock is to keep a simple testing notebook, digital or paper, for every material you use. For each entry record the supplier, thickness, color, and the exact power, speed, DPI, and pass count that worked, plus a short note on edge quality and smell. Within a month you will have a personal reference far more useful than any generic chart, because your machine and your batches are unique.
Test squares are the habit that makes this work. Cut a small grid of varying settings into a scrap offcut and label it with the results, then clip that square to the notebook page. Next time you buy the same plywood or acrylic, you skip the guesswork and go straight to a known-good preset. This pays for itself the first time you avoid ruining a $15 blank.
Also note failures, not just wins. If a certain leather scorched or a plastic melted badly, write it down so you do not repeat the mistake when you are in a rush with an order deadline. Over time your notebook becomes your shop's most valuable asset, and it lets you train a helper or hand off production without losing consistency across batches.
Reading Safety Data Before You Cut
Before committing to any new sheet or blank, spend a minute checking what it actually is. Many craft materials arrive without clear labeling, and a quick search for the supplier's safety data sheet tells you whether it is laser-safe. If a material contains chlorine, fluorine, or epoxy resins you cannot identify, treat it as unsafe until proven otherwise. This five-minute check protects your lungs, your optics, and your machine warranty, and it becomes second nature once you build a trusted supplier list. Pair it with the testing notebook from the previous section so every new material gets both a safety verdict and a proven setting before it ever touches your bed.
FAQ
Can a CO2 laser cut metal? Standard CO2 lasers do not cut bare metal because it reflects the infrared beam. They can mark coated or anodized metals, and specially treated steel, but cutting steel or aluminum needs a fiber laser instead.
Why does my acrylic edge look cloudy? Cloudy edges usually mean too little air assist or too high a speed, letting vaporized plastic resettle. Increase air assist, slow slightly, and use cast acrylic for the clearest polished cut.
Is MDF safe to laser? MDF cuts and engraves well and is cheap for practice, but it produces fine dust and formaldehyde-containing fumes, so run strong ventilation and a good mask when handling the raw sheet.
Start Exploring Materials with Confidence
Mastering a small set of reliable CO2 laser materials is the fastest path from nervous beginner to confident maker. Pick wood, acrylic, and leather as your core trio, test every new batch with a scrap square, and keep a notebook of the settings that worked. If you later outgrow a desktop bed, HF Laser (https://www.hflaser.com/laser-cutter.html) builds larger flatbed and auto-feeding CO2 machines for scaling production.
- National hotline: +86-531-86516855/56/57
- Enterprise mailbox:sales@redsaillaser.com
- Address: Room 402E, Tower D, Yinhe Building, 2008 Xinluo Avenue, Shunhua Road Subdistrict, Jinan Area, China (Shandong) Pilot Free Trade Zone


Redsail Tech Co. © 2002-2026. All Rights Reserved.