
Nothing ruins a project faster than a cut that looks perfect on the left edge and drifts a millimeter off by the right. Straight, repeatable cuts are the foundation of every good laser project, whether you are making a box that needs to fold flat, a sign with crisp corners, or a batch of coasters that all have to match. The good news is that most cutting drift is not a fault in the machine itself — it is a calibration problem you can fix in an afternoon with basic tools and a patient afternoon.
In this guide we will walk through the practical steps that keep a CO2 laser cutting true: squaring the gantry, setting belt tension, aligning the work bed, and proving it all with a test pattern. These checks apply to desktop units like the M4060E Cyclone and M3050 Breeze as well as larger beds such as the CM1390E Elite, and they will save you far more material than the time they take. Treat calibration as routine maintenance, not a rescue mission, and your cut quality stays predictable.
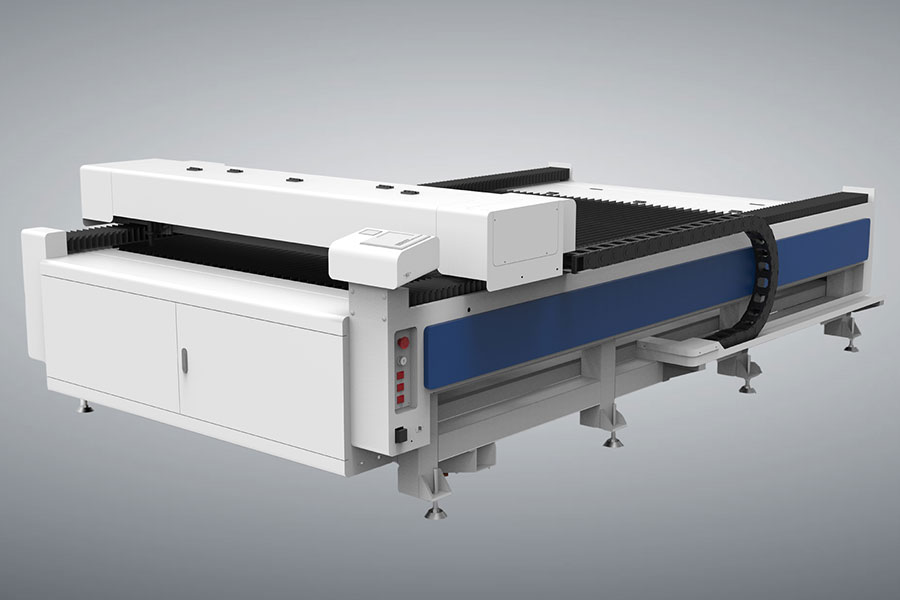
Why Straight Cuts Start with a Square Gantry
The gantry is the beam that carries the laser head left and right while the bed moves front to back. If that beam is not perfectly perpendicular to the rails, every horizontal line becomes a shallow wedge and every rectangle becomes a parallelogram. This is the single most common cause of "my cuts are crooked" complaints, and it shows up most on long parts and on jobs that span the full width of the bed where even a tiny angle is magnified over distance.
Squaring the gantry is a mechanical adjustment, not a software one. On most Redsail machines the gantry is held by two carriages, and one side has adjustable mounting holes or eccentric nuts. The goal is simple: measure the distance from the front rail to the gantry at the left and right ends, and make those two numbers identical. A 1 mm difference across a 900 mm bed is enough to throw a 300 mm part visibly out of square, so precision here pays off.
Do this with the machine powered off and the head parked at a known position. Use a reliable steel ruler or, better, a pair of digital calipers with a depth probe. Adjust one side at a time, re-measure, and repeat until both readings match within half a millimeter. Once the gantry is square, resist the urge to move it again — most later drift comes from bumping the carriage while cleaning the rails or changing a focus lens.
Checking and Tuning Belt Tension
Belts translate motor motion into head movement, and a loose or unevenly tensioned belt stretches under load, so the head lags behind where the controller thinks it is. The result is wavy cuts, rounded corners, and a part that is slightly smaller than designed. Belt tension is the quiet hero of accurate cutting, and it deserves a dedicated check rather than a casual tug.
Here is a quick routine you can repeat monthly:
- Press gently on the X and Y belts with a fingertip. They should feel firm and spring back, not floppy or drum-like.
- Listen for a low "thrum" when you pluck them; a healthy belt sounds like a low guitar string, not a slack rubber band.
- Check tension on both ends of each axis. A belt can be tight at the motor and loose at the idler, which causes direction-dependent drift.
- Retension by small increments. Over-tight belts wear bearings and add noise without improving accuracy.
If your machine uses a known-good controller such as a Ruida board, you can also watch the reported position in the software after a commanded move to confirm the head lands where expected. That feedback loop turns guesswork into measurement and helps you catch a slipping pulley before it ruins a paid job.
Bed Alignment and Material Placement
Even a perfectly squared machine will cut crooked if the material is not aligned to the bed. Bed alignment is as much about your habits as the hardware. A sheet of plywood that sits at a five-degree angle might cut fine on its own, but the moment you try to nest a second part against it, everything shifts and your registration falls apart.
Start every job by squaring your stock to the honeycomb or blade bed using the front-left corner as your reference. Many makers cut a thin "fence" strip and leave it glued or taped to the bed so material always butts against a true edge. For repeat work, a magnetic or L-shaped jig does the same job and speeds setup dramatically, especially when you are cutting dozens of identical blanks.
Also watch the focus height. A beam that is focused above or below the surface widens the kerf and can make a straight line look fuzzy or tapered. Run a focus ramp test on scrap before a production run, and re-check after changing material thickness. Combined with a squared gantry, good focus is what separates a clean edge from a ragged one.
Running a Calibration Test Pattern
The only way to know your machine is cutting true is to measure it. A laser calibration test pattern turns adjustment into evidence. You do not need fancy software — a simple set of shapes does the job and takes only a few minutes to draw and cut.
Draw a rectangle that spans most of the bed, a long diagonal line from corner to corner, and a grid of small squares. Cut them in a scrap piece of the same material you plan to use. Then measure:
- The rectangle's opposite sides should be equal in length.
- The two diagonals should be equal; unequal diagonals mean the bed is not square.
- The grid squares should all be the same size; graduated sizes point to belt stretch or a slipping pulley.
Keep the test cut as a reference. When a future job drifts, re-run the pattern first — it takes five minutes and tells you exactly which axis to chase before you start loosening bolts. Over time you will recognize the signature of each problem, which makes diagnosis almost instant.
Corner-to-Corner Accuracy Across the Whole Bed
The real test of straight cuts is consistency from one corner of the bed to the opposite one. Many machines cut beautifully in the center and drift at the extremes, especially on larger beds like the CM1325 or CM1625 where the gantry travels a long distance and small errors accumulate.
To check, cut the same small square in all four corners and the center. Measure each. If corner squares differ from the center by more than your tolerance, look at the rails: they may need cleaning, the carriages may have worn wheels, or the bed may be slightly twisted in its frame. A long straightedge laid along each rail will reveal a bow you cannot see by eye. On bigger beds, shimming the leg that sits low often restores flatness better than any software tweak.
This corner-to-corner discipline matters most when you panelize a large design. A sign that is perfectly square in the middle but skewed at the ends will show a visible gap when the pieces are assembled, and that is exactly the kind of defect a careful buyer or Etsy customer will notice immediately.
A Simple Maintenance Schedule
Calibration is not a one-time event. Heat, vibration, and cleaning all nudge settings over time. A light routine keeps cuts honest:
- Weekly: wipe rails, check belt feel, confirm focus.
- Monthly: square-check the gantry and run a quick test pattern.
- Quarterly: inspect pulleys for set-screw slip and re-tension belts.
Pair this with a logbook of readings. When a cut goes wrong, the log shows whether the gantry crept or a belt loosened, and you fix the right thing instead of chasing ghosts. Makers who keep a simple spreadsheet of dates and measurements almost always solve drift problems in minutes rather than hours.
Frequently Asked Questions
Q: How often should I square my laser gantry?
A: For a home or Etsy-scale shop, a full square check once a month is plenty, plus a quick visual and belt-feel test each week. If you move the machine, bump the gantry while cleaning, or change belts, square it again before the next job. Busy production shops running daily should check every week to keep tolerances tight.
Q: Why are my cuts straight in the middle but crooked at the edges?
A: That pattern usually points to a twisted bed, a bowed rail, or belt tension that differs between the two ends of an axis. Run corner test squares and a diagonal check. If corners differ from the center, inspect the rails with a straightedge and shim the low leg. If one axis is worse than the other, focus on that belt first.
Q: Can software fix a mechanically crooked cut?
A: Software can compensate for small, consistent errors, but it cannot fix a gantry that is out of square or a slipping belt. Mechanical squaring and belt tension should always come first; treat firmware or software offsets as fine-tuning only, not a cure for the root cause.
When your cuts run true, every other part of your workflow gets easier — nesting, batching, and finishing all become predictable. If you are shopping for a machine that holds calibration well out of the box, the Redsail lineup from the compact M3050 Breeze to the CM1390E Elite is worth a close look, and you can compare builds and bed sizes at https://www.redsaillaser.com/Laser-Cutter.html.
If you want to see how other CO2 cutter brands approach bed size and calibration support, take a look at HF Laser's full cutter range before you decide.

- National hotline: +86-531-86516855/56/57
- Enterprise mailbox:sales@redsaillaser.com
- Address: Room 402E, Tower D, Yinhe Building, 2008 Xinluo Avenue, Shunhua Road Subdistrict, Jinan Area, China (Shandong) Pilot Free Trade Zone


Redsail Tech Co. © 2002-2026. All Rights Reserved.