When Cuts Lean, Something Moved
A CO2 laser cuts straight only when the beam travels true and the gantry moves square. After shipping, an accidental bump, or months of steady use, one of those two things drifts and your once-clean edges start to lean to one side. The fix is methodical, not mysterious: check the beam path, square the axes, tension the belts, then prove the work with a deliberate test cut.
Do this once and you restore the accuracy the machine had on day one. Skip it and you keep reaching for the sandpaper to true up crooked parts, which costs more time than the calibration ever would, and it still leaves you with a part that was never cut right in the first place.
Gather Tools and Work Safe
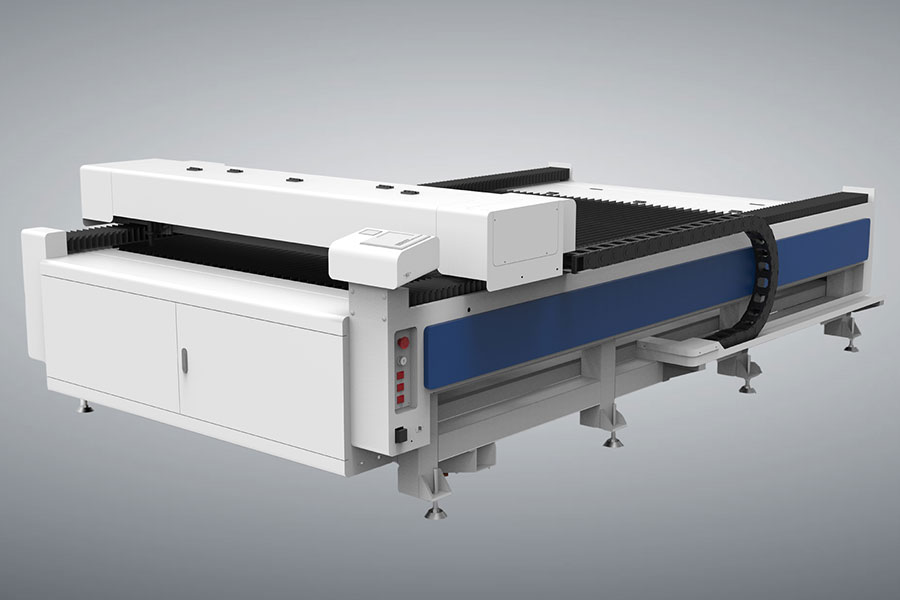
Before you touch a single mirror, set yourself up so the job goes smoothly and nobody gets hurt. You will want a roll of masking tape, a few small squares of card stock or thermal paper to catch the beam pulse, a carpenter's square or a long metal ruler, an allen key set that fits your frame hardware, and a soft lint-free cloth for wiping optics. A notebook or a maintenance card to log settings is worth its weight for the next calibration session.
Safety comes first because you are working around an invisible, high-power beam. Never look directly into the path, keep the lid closed and the interlock engaged whenever the tube is firing, and wear proper eye protection rated for the laser's wavelength if you must open the enclosure for mirror work. Power the machine down at the wall before you loosen frame bolts so a stray command cannot move the gantry while your fingers are near it.
Also confirm the honeycomb bed itself is level and clean before you begin. A bed that has warped or collected debris gives a false reference, so sweep it out and, if your machine allows, jog the head to the four corners to confirm it sits evenly. Calibration measured against a crooked bed simply bakes the error into every later job.
Step 1: Pulse the Beam Path
With the machine safe and the lid closed for a test, fire low-power pulses at a target taped to each mirror in turn. The burn should land dead center on every mirror; if it sits off to one side, that mirror needs adjusting. Work from the tube outward, centering each one before moving to the next, because a misaligned first mirror simply pushes the error down the line to the others.
A centered beam means the energy travels straight down the column and out through the head with no clipping. An off-center beam hits the edge of the nozzle and your cuts weaken and wander exactly where the beam clips the aperture. Take your time here; the mirror alignment is the foundation that every later step assumes is already correct, and rushing it only hides a fault that returns as crooked work.
Pulse at more than one point along each axis rather than a single shot, because a mirror can read centered at the home position yet drift as the head travels. Compare the entry and exit burns on a longer tape strip so you can see the trend, not just a single dot, and adjust until the beam holds center from one end of the travel to the other.
Step 2: Square the Gantry
The X axis must sit at a right angle to the Y rails or every cut leans. Many frames have adjustment screws or eccentric nuts at the ends of the gantry; loosen them, square the assembly against a known reference — a carpenter's square laid on the bed or a measured diagonal between opposite corners — and then retighten. Re-check both corners, because a frame can read square at one end and be twisted at the other.
If your controller supports it, a software squareness offset can compensate a tiny residual error, but fix the hardware first. Software cannot make up for a physically twisted frame, and leaning on a digital fudge factor only hides a problem that will grow. Measure the two bed diagonals; they should match within a millimeter on a small machine, and once they do you have a reliable reference to cut against for straight cut fix work.
Mark your reference square's position with a piece of tape so you can repeat the check exactly next month. Consistent setup is what makes laser calibration trustworthy over time, because a measurement taken differently each session produces different numbers and leaves you guessing whether the machine actually moved.
Step 3: Tension the Belts
Loose belts stretch under load and the head lags behind the command, so circles become eggs and long straight cuts bow inward. Each belt should feel taut with a slight give when you pluck it — not drum-tight and not floppy. Tighten the idler or the tension screw a turn at a time and re-test; over-tight belts wear the bearings and add noise you will hear on every job.
Listen while the machine cuts. A belt that slaps, whines, or chatters is telling you it is loose or riding off its pulley. Quiet, even motion is the goal, and a belt that moves smoothly is one that will hold its calibration between checks. If a belt looks frayed or glazed rather than clean, replace it instead of re-tensioning a worn part, because a tired belt will never hold belt tension the way a fresh one does.
While you are at the belts, check the pulley set screws on the stepper motors. A set screw that has backed out lets the pulley slip a fraction on the shaft, which produces exactly the kind of intermittent drift that passes one test and fails the next. A dab of threadlocker on a properly seated screw keeps it put for the long run.
Step 4: Prove It With a Test Cut
Cut a square and a circle from scrap and measure both with a real square and calipers. The square's corners should read 90 degrees and opposite sides should be equal; the circle should close cleanly with no flat spot where the head hesitated. If the square comes out a parallelogram, the gantry is still off, and if the circle shows a step, a belt or pulley is slipping under load.
Keep that test cut as a reference piece taped to the wall or inside the lid. Re-run it monthly or after any move, and you will catch drift before it ever reaches a paying customer's order. A five-minute proof cut is cheaper than the goodwill you lose shipping a crooked batch, and it is the clearest proof your square laser cuts are back to spec.
Use calipers rather than eyeballing the square, because a single degree of error is invisible to the naked eye yet visible in a fitted joint. Define your tolerance up front — for most maker work, corners within half a degree and sides within a few tenths of a millimeter are plenty — and only sign off the machine when it meets that standard.
Step 5: Log, Maintain, and Repeat
Write the date and any changes in a maintenance card taped inside the lid so the next session starts where this one ended. Laser calibration is not a one-time event; it is a habit. A short monthly check prevents the slow creep that eventually turns into a ruined run and an unhappy buyer who noticed the lean.
Pair the calibration with a lens and mirror wipe, because a dirty optic scatters the beam and mimics an alignment fault. Clean first, then square, so you are not chasing a ghost that is really just a film of residue on the lens. Good belt tension, a true gantry, and clear optics together are what make square laser cuts reliable day after day, and that reliability is what lets you take on tighter-tolerance work with confidence.
Note the seasons in your log, because temperature and humidity swings can shift a frame slightly between winter and summer. A machine that was perfect in January may need a light re-square by July, and a dated record tells you whether the change is real drift or just normal environmental movement you can correct in minutes.
FAQ
Why is only one corner of my square off?
Almost always the gantry is not square at that end. Re-square it against a reference and re-measure both corners before trusting the machine again.
Can software fix a crooked cut?
A small offset, yes; a physically twisted frame, no. Always fix the hardware first, then fine-tune any tiny residual error in software.
How often should I calibrate?
After shipping or any move, and monthly during normal use. Busy shops that cut all day often benefit from checking every few weeks.
Get Started
Pulse-center the mirrors, square the gantry, tension the belts, and prove it with a test square. Straight cuts return the same day. For volume cutting once calibrated, industrial flatbed CO2 lasers at HF Laser keep the accuracy at scale.
- National hotline: +86-531-86516855/56/57
- Enterprise mailbox:sales@redsaillaser.com
- Address: Room 402E, Tower D, Yinhe Building, 2008 Xinluo Avenue, Shunhua Road Subdistrict, Jinan Area, China (Shandong) Pilot Free Trade Zone


Redsail Tech Co. © 2002-2026. All Rights Reserved.